Freezer evaporators are essential components in refrigeration systems, responsible for absorbing heat from the interior of a freezer and facilitating the cooling process. As a B2B buyer, your primary concerns when selecting a freezer evaporator may include its efficiency, compatibility with your existing systems, and overall reliability. This article will guide you through the critical factors to consider when choosing a freezer evaporator, evaluating its quality, sourcing reliable suppliers, understanding its applications across industries, and addressing common issues you may encounter.
When selecting a freezer evaporator, several key factors should be evaluated:
Capacity Requirements: Determine the cooling capacity needed for your application. This is typically measured in BTUs (British Thermal Units) and should align with the size of your freezer and the expected load.
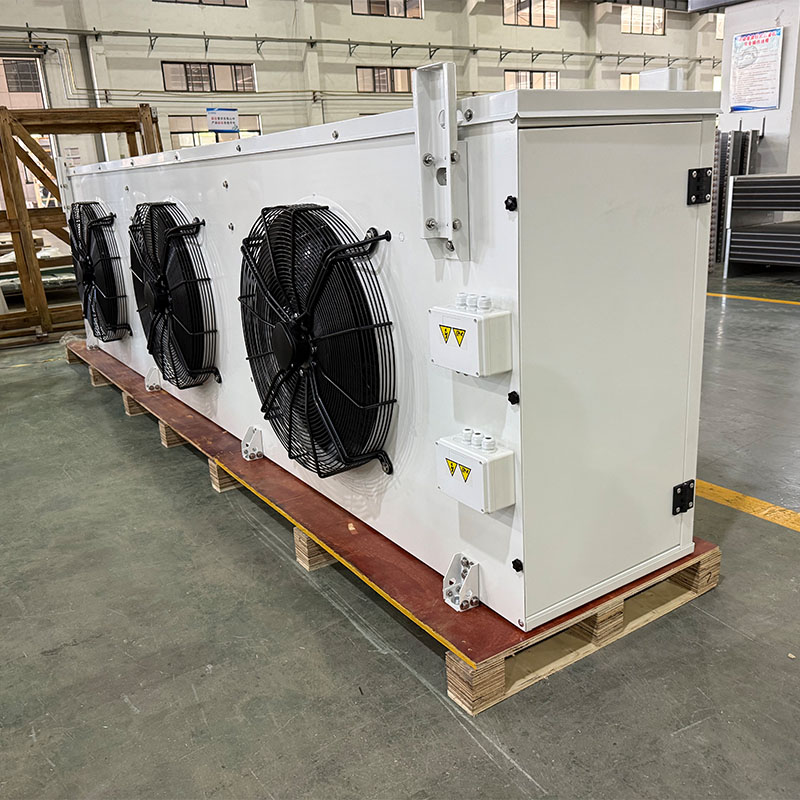
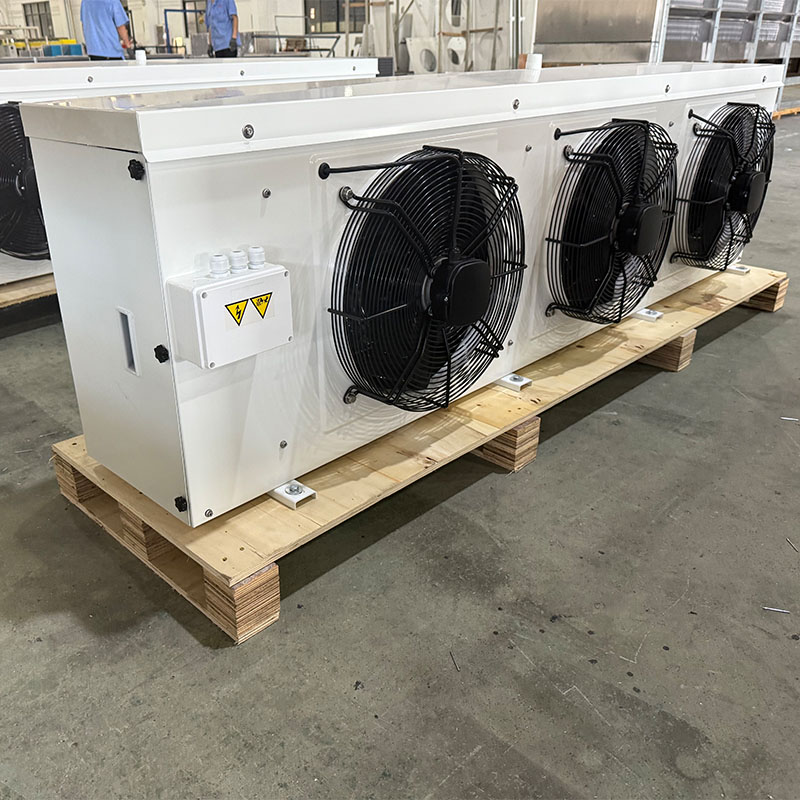
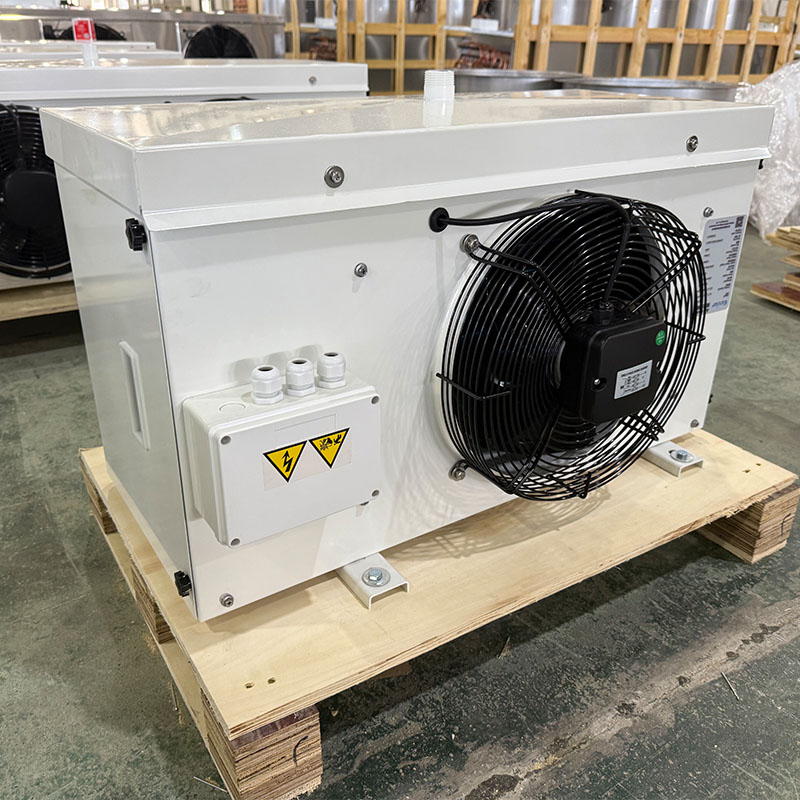
Design Configuration: Freezer evaporators come in various configurations, including finned-tube, flat plate, and air-cooled designs. The choice of configuration should depend on the specific cooling needs and space constraints of your project.
Material Selection: The materials used in the evaporator can significantly affect durability and performance. Common materials include galvanized steel, aluminum, and stainless steel. Assess the environmental conditions, such as humidity and temperature, to choose the most suitable material.
Energy Efficiency: Look for evaporators that offer high energy efficiency ratings. This not only reduces operational costs but also contributes to a more sustainable operation. Consider using Evaporators that meet these criteria for optimal performance.
Customization Options: Depending on your specific requirements, you may need to consider custom designs or modifications. Evaluate potential suppliers’ capabilities to accommodate these needs.
By evaluating these factors, you can ensure that the freezer evaporator you select will meet your project’s requirements effectively.
When purchasing freezer evaporators in bulk, quality assurance becomes paramount. Here are several aspects to consider:
Certifications and Standards: Ensure that the evaporators comply with relevant industry standards and certifications, such as CE or UL. This not only assures quality but also indicates adherence to safety protocols.
Warranty and Support: A reliable supplier should offer a robust warranty for their products and be available for after-sales support. This is crucial for addressing any issues that may arise post-purchase.
Quality Control Processes: Inquire about the manufacturer’s quality control measures. This can include testing protocols, inspection processes, and the use of advanced manufacturing techniques that ensure product consistency.
Material Quality: Evaluate the specifications related to the materials used in the evaporators. High-quality materials enhance durability and performance, while inferior materials may lead to faster degradation and operational issues. Selecting high-quality Refrigeration Accessories can also contribute to overall system reliability.
Sample Approval: Before committing to a large order, request samples to verify performance. Testing these samples under actual operating conditions can reveal potential issues that may not be apparent from specifications alone.
By focusing on these quality indicators, you can make informed decisions that minimize risk and enhance the reliability of your refrigeration systems.
Sourcing reliable freezer evaporators involves identifying reputable manufacturers and suppliers. Consider the following strategies:
Industry Trade Shows: Participating in refrigeration and HVAC trade shows can provide direct access to manufacturers. This allows you to assess products firsthand and establish relationships with suppliers.
Online Marketplaces and Directories: Utilize B2B platforms like Alibaba, ThomasNet, or industry-specific directories to find manufacturers. Look for those with positive reviews, a solid track record, and verified credentials.
Referrals and Networking: Consult with industry peers or professional networks for recommendations on trusted suppliers. Personal testimonials can often lead to reliable sources.
Manufacturer Background: Research the manufacturer’s history, experience, and technological capabilities. Established companies, like Shanghai EMTH, with over 20 years in the refrigeration equipment sector, often have proven reliability and innovation.
Lead Time and MOQ: Confirm the lead times and minimum order quantities (MOQ) offered by suppliers. This can help you align your purchasing strategy with your operational needs.
By employing these sourcing strategies, you can find reliable suppliers that meet your business requirements effectively.
Freezer evaporators are versatile components used across various industries. Here are some of their best applications:
Food and Beverage Industry: In supermarkets and cold storage facilities, freezer evaporators are crucial for preserving perishable items. They are used in display cases, walk-in freezers, and commercial refrigeration units.
Pharmaceutical Industry: These evaporators are essential in maintaining the required temperature for sensitive pharmaceuticals and vaccines, ensuring their efficacy and safety.
Cold Chain Logistics: In transportation and storage, freezer evaporators help maintain optimal temperatures for perishable goods, preventing spoilage during transit.
Ice Cream and Dairy Production: In manufacturing facilities, evaporators play a vital role in the production process, ensuring the correct temperature for freezing and storing dairy products.
Industrial Applications: In manufacturing settings, freezer evaporators can be used for cooling processes in various applications, including chemical production, where temperature control is critical for product integrity.
Understanding the specific applications of freezer evaporators can help you identify the right product for your needs.
More than 20 years of' experience and an experienced EMTH R&D staff.
EMTH EMTH has a solid track record in the field, with over 3,000+ happy customers.
The modern factory has an area greater than 40,000 square meters, to satisfy the majority of the EMTH production requirements.
Complete service program, from formulating of plans to the production and Cooling room, to after-sales service, there are specific docking.

Welcome to EMTH, a cold storage refrigeration equipment specialist in China! We offer innovative and effective cold storage solutions, including cold storage, evaporator, condensing unit and ice machine.
Room 304-305B, Building 5, BESHINE B.P, No. 559Zhuyuan Road, Minhang District 201112, Shanghai, China
Copyright © Shanghai EMTH Import & Export Co., Ltd. All Rights Reserved. - Privacy Policy
 EN
 AR
 BG
 HR
 CS
 DA
 NL
 FI
 FR
 DE
 EL
 IT
 JA
 KO
 NO
 PL
 PT
 RO
 RU
 ES
 TL
 IW
 ID
 LT
 SR
 VI
 HU
 TH
 MS
 AZ
 JW
 LO
 MN
 SO
 MY
 KK
 TG
 UZ
 GD
 XH