Choosing the right evaporator unit for a walk-in freezer is crucial for maintaining optimal temperature and efficiency in refrigeration applications. These units play a vital role in the preservation of perishable goods, making their selection a top priority for purchasing managers and facility engineers. This article will guide you through the key specifications, quality evaluation, bulk order options, installation guidance, and cost factors to consider when purchasing evaporator units for walk-in freezers.
When selecting an evaporator unit for a walk-in freezer, several key specifications must be considered:
Cooling Capacity: Measured in BTUs (British Thermal Units), the cooling capacity must match the size and insulation properties of your freezer. A unit with insufficient capacity will fail to maintain the desired temperature, while an oversized unit can lead to inefficient cycling and increased energy costs.
Airflow Design: The evaporator's airflow design—whether it is fan-forced or gravity—affects how effectively cold air is distributed throughout the freezer. Fan-forced models provide more uniform cooling, which is often preferable for larger or high-traffic freezers.
Material Construction: High-quality evaporator units typically feature corrosion-resistant materials such as stainless steel or treated aluminum. This construction is vital for durability and longevity, especially in environments with high humidity.
Temperature Range: Ensure that the evaporator unit is capable of operating within the desired temperature range, typically between -10°F to 0°F for walk-in freezers. Confirm this specification aligns with your application needs.
Defrosting Method: Choose between automatic or manual defrost options. Automatic defrost systems can save time and labor, while manual systems may be more cost-effective for smaller operations. Additionally, consider integrating an Evaporator that aligns with your defrosting preferences for better efficiency.
Understanding these specifications will help you make an informed decision that meets your refrigeration needs effectively.
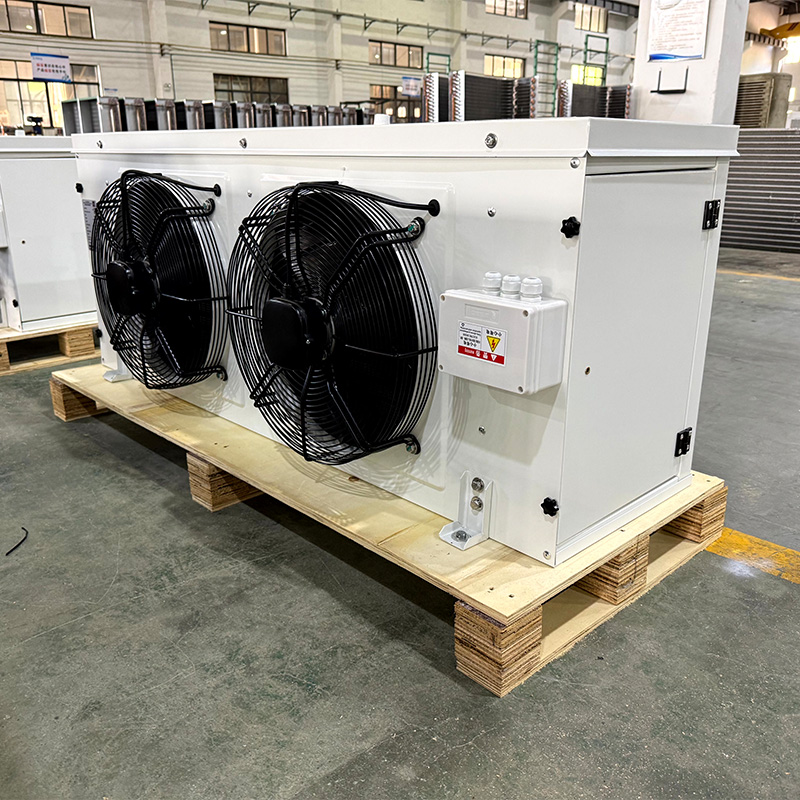
Evaluating the quality of evaporator units is essential to ensure reliability and efficiency. Consider the following factors:
Manufacturer Reputation: Research the manufacturer’s history, experience, and customer reviews. Companies with a long-standing reputation, such as Shanghai EMTH with over 20 years in refrigeration equipment, typically have established quality control processes and product reliability.
Certifications: Look for certifications such as ISO or CE, which indicate that the product meets international quality and safety standards. These certifications can provide additional assurance of the unit's quality.
Warranty and Support: A robust warranty and responsive customer support can be a good indicator of the manufacturer's confidence in their product. Ensure the warranty covers key components and that support is readily available for troubleshooting.
Sample Approval: Before committing to a bulk order, request a sample unit for testing. Evaluate it under actual operating conditions to ensure it meets performance expectations.
Quality Control Processes: Inquire about the quality control measures implemented during manufacturing. A manufacturer that conducts rigorous testing and inspection will likely produce more reliable products.
Taking the time to evaluate these quality indicators will help you select an evaporator unit that delivers consistent performance and meets your operational standards.
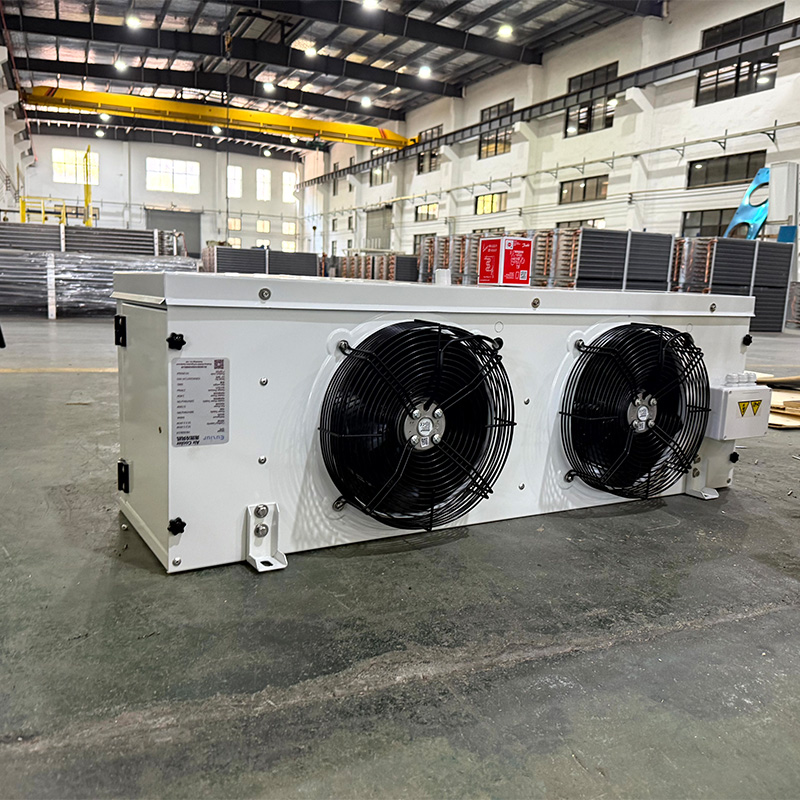
When considering bulk orders for evaporator units, several factors come into play:
Minimum Order Quantity (MOQ): Manufacturers often have a minimum order quantity that can affect pricing and availability. Understanding the MOQ will help you plan your inventory needs accordingly.
Pricing Structure: Bulk orders may qualify for discounts. Discuss pricing tiers with the manufacturer to ensure you receive the best possible deal based on your order size.
Customization Options: Larger orders may allow for customization of evaporator units to better suit your specific application. This can include adjustments in size, cooling capacity, or additional features like enhanced insulation.
Lead Time: Confirm the lead time for bulk orders as it may vary based on production schedules and the complexity of your order. Planning ahead can help avoid unexpected delays in your operation.
Shipping and Handling: Understand the shipping options available and any associated costs. Some manufacturers may offer free shipping for large orders, while others may charge additional fees. Additionally, inquire about the availability of Refrigeration Accessories that may be needed for your order.
By clarifying these options, you can better prepare for ordering and ensure your facility is equipped with the necessary refrigeration solutions.
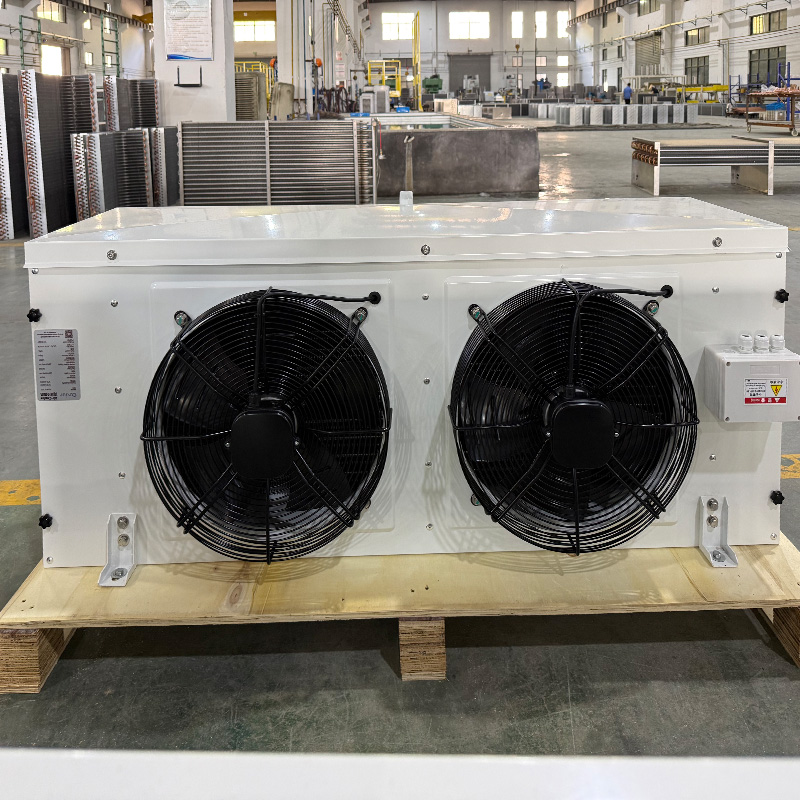
Proper installation of evaporator units is crucial for optimal performance. Consider the following steps:
Site Assessment: Before installation, conduct a thorough site assessment to determine the best location for the evaporator unit. Ensure it is positioned to allow for proper airflow and accessibility for maintenance.
Electrical Connections: Verify that the electrical connections meet the specifications required by the evaporator unit. Improper connections can lead to operational issues or damage to the unit.
Mounting and Support: Ensure the evaporator unit is securely mounted and supported according to the manufacturer’s guidelines. This prevents vibrations and potential damage during operation.
Refrigerant Lines: Connect the refrigerant lines according to the manufacturer's instructions. Proper insulation of these lines is essential to maintain efficiency and prevent condensation.
System Testing: Once installed, conduct a thorough system test to check for leaks and ensure the unit operates within the specified temperature range. Monitoring the system after installation will help identify any issues early on.
Following these installation guidelines will help ensure that the evaporator unit operates efficiently and effectively within your walk-in freezer.
With more than 20 years of knowledge, we've developed a a complete production and sales and after-sales system with more than 20 patent certificates and a highly skilled R&D EMTH team.
EMTH has a long-standing track record of success in the industry with more than 3,000 satisfied customers.
Complete service program, from formulating of plans, production of Cold room as well as project landing until after-sales service, there are specific docking.
The modern factory has an area greater than 40,000 square meters, to satisfy the majority of the EMTH production requirements.

Welcome to EMTH, a cold storage refrigeration equipment specialist in China! We offer innovative and effective cold storage solutions, including cold storage, evaporator, condensing unit and ice machine.
Room 304-305B, Building 5, BESHINE B.P, No. 559Zhuyuan Road, Minhang District 201112, Shanghai, China
Copyright © Shanghai EMTH Import & Export Co., Ltd. All Rights Reserved. - Privacy Policy
 EN
 AR
 BG
 HR
 CS
 DA
 NL
 FI
 FR
 DE
 EL
 IT
 JA
 KO
 NO
 PL
 PT
 RO
 RU
 ES
 TL
 IW
 ID
 LT
 SR
 VI
 HU
 TH
 MS
 AZ
 JW
 LO
 MN
 SO
 MY
 KK
 TG
 UZ
 GD
 XH