Industrial evaporators are crucial components in the refrigeration systems of walk-in freezers, designed to efficiently remove heat from the refrigerated space. When selecting an industrial evaporator for walk-in freezers, B2B buyers, including purchasing managers, engineers, and product managers, have specific concerns regarding performance, compatibility, and reliability. This article will help you understand how to evaluate the quality of these evaporators, troubleshoot common problems, adhere to installation guidelines, select the right unit for your project, and comprehend the advantages of various materials used in their construction.
When assessing the quality of industrial evaporators for walk-in freezers, several key specifications should be taken into account:
Heat Exchange Efficiency: Look for evaporators with a high coefficient of performance (COP) which indicates their efficiency in converting energy into cooling power. This metric is critical for reducing operational costs.
Material Integrity: Evaporators are often made from materials like copper or aluminum due to their excellent thermal conductivity. Ensure that the material chosen can withstand the specific conditions of your application, including temperature fluctuations and exposure to moisture. For instance, refrigeration accessories can enhance the overall functionality of the system.
Design and Construction: Evaluate the design for features such as fin spacing and surface area. Fins increase the surface area for heat exchange, which can enhance cooling capacity. Additionally, check for adequate insulation to minimize energy loss.
Certifications and Standards: Quality certifications and compliance with industry standards, such as ISO or CE, can serve as indicators of a manufacturer’s commitment to quality.
Manufacturer’s Experience: Companies with extensive experience, like Shanghai EMTH, which has over 20 years in refrigeration equipment manufacturing, are often more reliable. Their expertise can lead to better product design and innovation.
By focusing on these factors, buyers can make informed decisions that align with their operational needs and budget constraints.
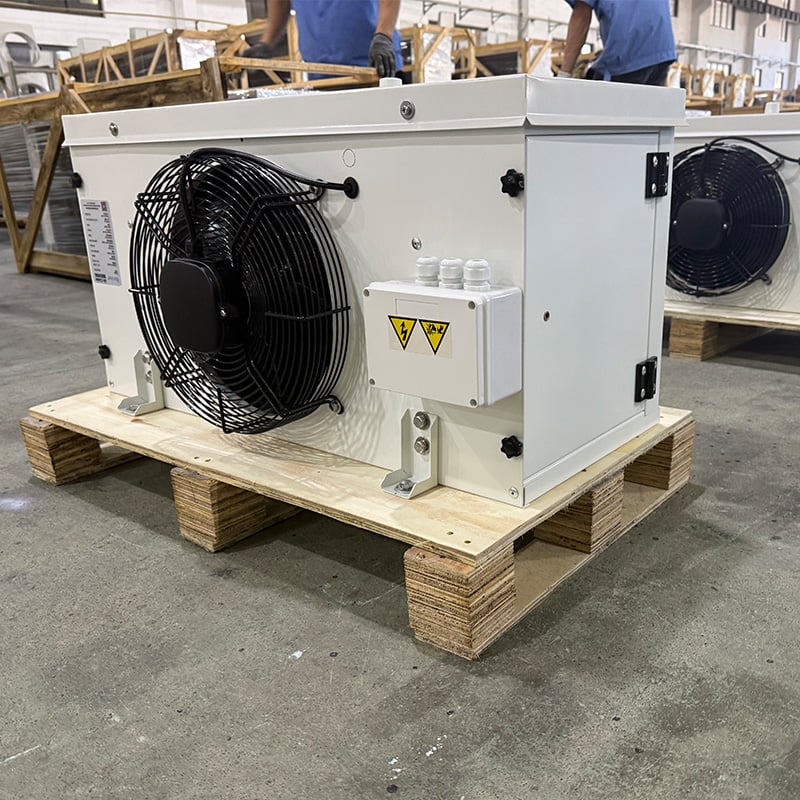
Walk-in freezer evaporators can encounter several common issues that affect their performance:
Frost Build-up: Frost accumulation on the evaporator coils can hinder efficiency. This often results from poor airflow or insufficient defrost cycles. Ensure that air circulation is unobstructed and consider programmable defrost controls to manage frost build-up effectively.
Inadequate Cooling: If the evaporator is not maintaining the desired temperature, check for refrigerant leaks, dirty coils, or improper sizing. Sizing the evaporator correctly for the space it serves is crucial; an oversized unit can lead to short cycling and inadequate dehumidification.
Noise Issues: Excessive noise may indicate a problem with the fan motor or imbalance in the fan blades. Regular maintenance and inspection should be part of your operational routine to ensure that moving parts are functioning correctly.
Corrosion: Evaporators in humid environments are at risk of corrosion. Using corrosion-resistant materials and coatings can help extend the life of the evaporator and maintain performance. Utilizing components like the Air Curtain can also help mitigate humidity issues.
By proactively addressing these issues, operators can minimize downtime and maintain optimal performance in their walk-in freezer systems.
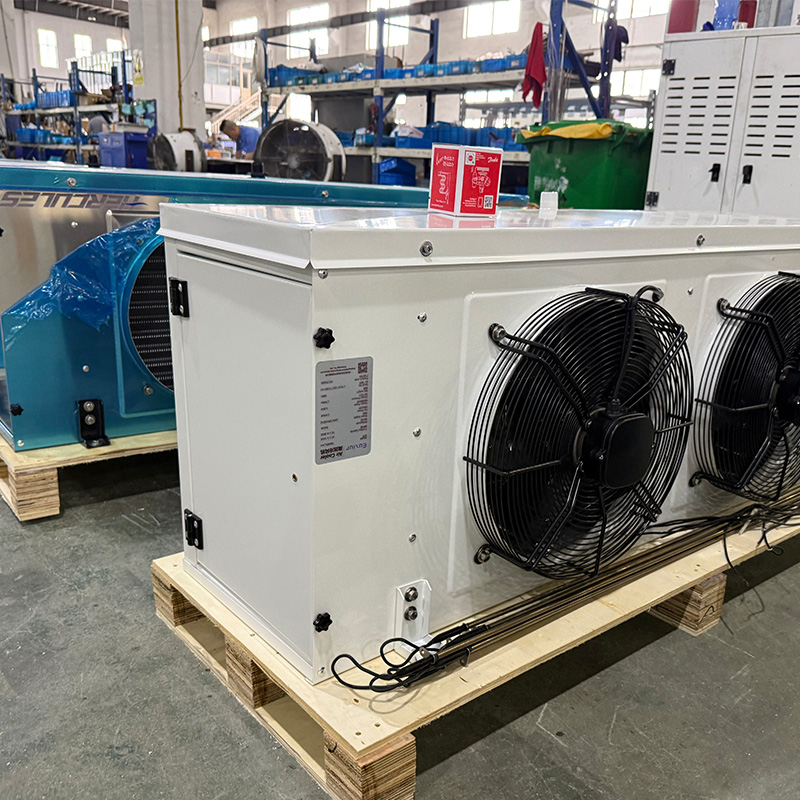
Proper installation of industrial evaporators is critical to ensure efficient operation. Here are some essential guidelines:
Location and Mounting: Install the evaporator in a location that allows for adequate airflow around the unit. This helps maintain efficient heat exchange and prevents overheating. Ensure that the unit is mounted securely to avoid vibrations that could lead to mechanical failure.
Alignment with Refrigeration System: The evaporator must be correctly aligned with the refrigeration system to ensure optimal refrigerant flow. Verify that the piping is correctly sized and insulated to minimize energy loss.
Electrical Connections: Follow the manufacturer’s guidelines for electrical connections. Ensure that all wiring is properly insulated and that the power supply matches the evaporator’s requirements to avoid electrical failures.
Testing: After installation, conduct thorough testing to ensure that the evaporator is functioning correctly. Check for leaks, proper airflow, and temperature control to confirm that everything is operating within specifications.
Adhering to these installation guidelines can significantly enhance the performance and longevity of the evaporator in your walk-in freezer.
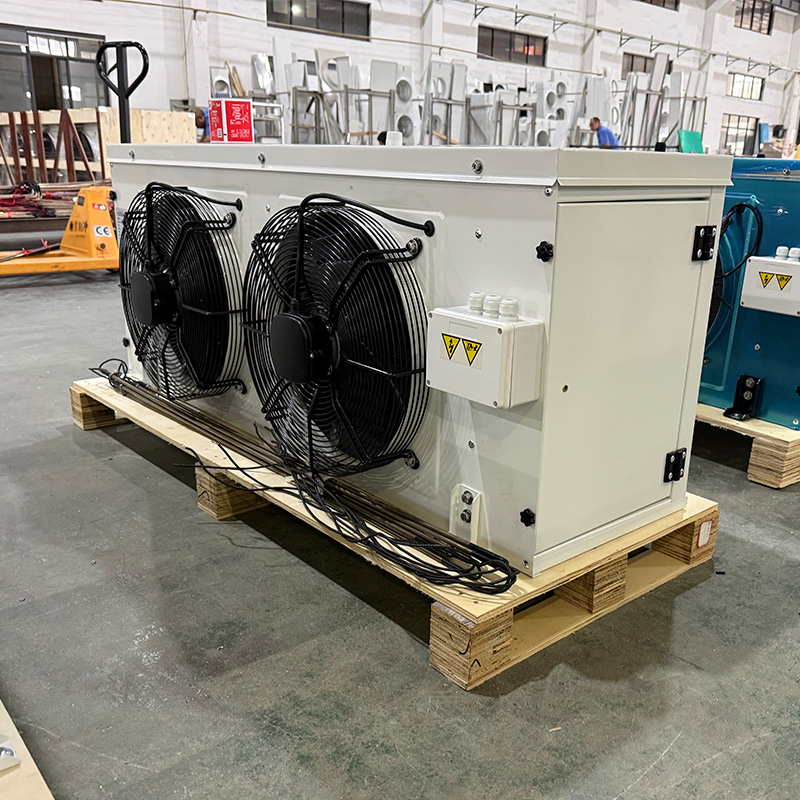
Choosing the right industrial evaporator for your walk-in freezer project depends on several factors:
Cooling Capacity: Determine the required cooling capacity based on the size and usage of your walk-in freezer. An undersized evaporator will struggle to maintain temperature, while an oversized unit can lead to inefficient operation.
Application-Specific Needs: Different applications may require specific types of evaporators. For instance, food storage may necessitate evaporators that handle high humidity levels, while pharmaceutical storage might require precise temperature control.
Customization Options: Many manufacturers, including Shanghai EMTH, offer customization options to tailor evaporators to specific needs. Inquire about features such as variable fan speeds or additional insulation to enhance performance.
Budget Considerations: While it can be tempting to choose the cheapest option, consider the total cost of ownership, including energy efficiency and maintenance needs. Investing in a quality evaporator can result in lower operational costs over time.
By evaluating these criteria, you can select the most suitable evaporator for your project, ensuring optimal performance and reliability.
The modern factory has an area greater than 40,000 square meters, to satisfy the majority of the EMTH production requirements.
With a great reputation in the business and over 3,000+ clients that they have served, EMTH EMTH is a trustworthy established supplier that is praised by its clients.
Special docking is offered for a complete service. This includes the design of Coldrooms, production installation, landing projects, and after-sales support.
With more than 20 years of knowledge, we've developed a a complete production and sales and after-sales system with more than 20 patent certificates and a highly skilled R&D EMTH team.

Welcome to EMTH, a cold storage refrigeration equipment specialist in China! We offer innovative and effective cold storage solutions, including cold storage, evaporator, condensing unit and ice machine.
Room 304-305B, Building 5, BESHINE B.P, No. 559Zhuyuan Road, Minhang District 201112, Shanghai, China
Copyright © Shanghai EMTH Import & Export Co., Ltd. All Rights Reserved. - Privacy Policy
 EN
 AR
 BG
 HR
 CS
 DA
 NL
 FI
 FR
 DE
 EL
 IT
 JA
 KO
 NO
 PL
 PT
 RO
 RU
 ES
 TL
 IW
 ID
 LT
 SR
 VI
 HU
 TH
 MS
 AZ
 JW
 LO
 MN
 SO
 MY
 KK
 TG
 UZ
 GD
 XH