An evaporator cold room is a specialized refrigeration system designed to maintain low temperatures for perishable goods. It effectively removes heat from the stored items, ensuring they remain fresh and safe for consumption. For B2B buyers, particularly purchasing managers and distributors, the primary concerns surrounding evaporator cold rooms include efficiency, reliability, and suitability for specific applications. This article will help you understand how to select the right evaporator cold room, the quality control measures to consider, supplier options, and the benefits of partnering with experienced manufacturers like Shanghai EMTH. Additionally, utilizing products like the Bitzer Condensing Unit can enhance the overall efficiency of your refrigeration system.
Selecting the right evaporator cold room hinges on several critical factors. First, assess the intended application. Different industries may require varying temperature ranges and humidity levels. For instance, food storage may necessitate a consistent temperature between -18°C to 0°C, while pharmaceutical applications could demand stricter temperature controls.
Next, consider the size and layout of the cold room. Dimensions should be based on the volume of goods to be stored, keeping in mind not just the quantity but also the types of products. A well-designed cold room allows for optimal airflow and space utilization, reducing the risk of spoilage. Incorporating components such as the YH Type Condenser can also contribute to better temperature regulation.
Material selection is another vital element. Insulation materials must be chosen for their thermal efficiency and durability, as they significantly impact energy consumption and operational costs. Polyurethane foam is a popular choice due to its excellent insulation properties and structural integrity. Ensure you choose a manufacturer that can customize materials based on your specific needs.
Lastly, confirm the evaporator's specifications, including the cooling capacity, which is usually measured in BTUs or kilowatts. This specification determines how quickly and efficiently the cold room can reach and maintain the desired temperature. A specialized manufacturer can provide guidance on the appropriate cooling capacity based on your application.
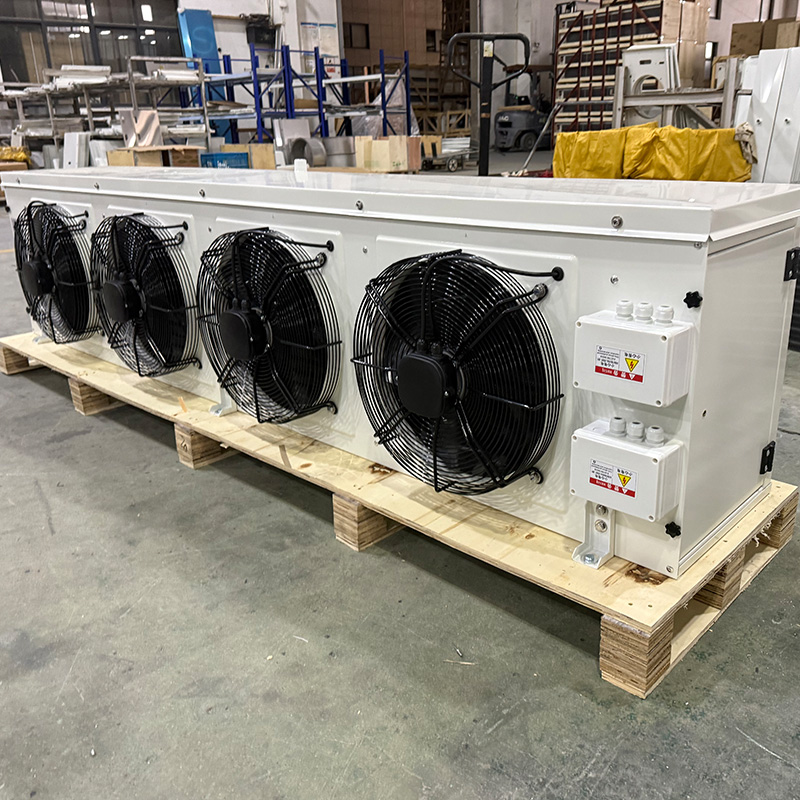
Quality control is paramount in the manufacturing of evaporator cold rooms. Start by ensuring that the manufacturing facility adheres to recognized standards, which may include ISO certifications or other relevant industry benchmarks. This ensures that the products are produced consistently and meet safety requirements.
A critical phase in production is the quality inspection of components, such as evaporators, condensers, and insulation materials. Each part should undergo rigorous testing to confirm its performance under operational conditions. For instance, testing the evaporator’s efficiency can reveal its ability to maintain temperatures and its energy consumption rates.
Before mass production, it’s advisable to approve a finished sample. This process helps verify that the dimensions, fit, and overall performance align with your operational needs. A sample can also be tested under actual operating conditions, allowing you to identify potential issues before full-scale production begins.
Regular audits and inspections during the production run can help ensure that quality standards are maintained. Buyers should also inquire about post-production quality checks and warranties offered by manufacturers, which can provide additional assurance of product reliability.
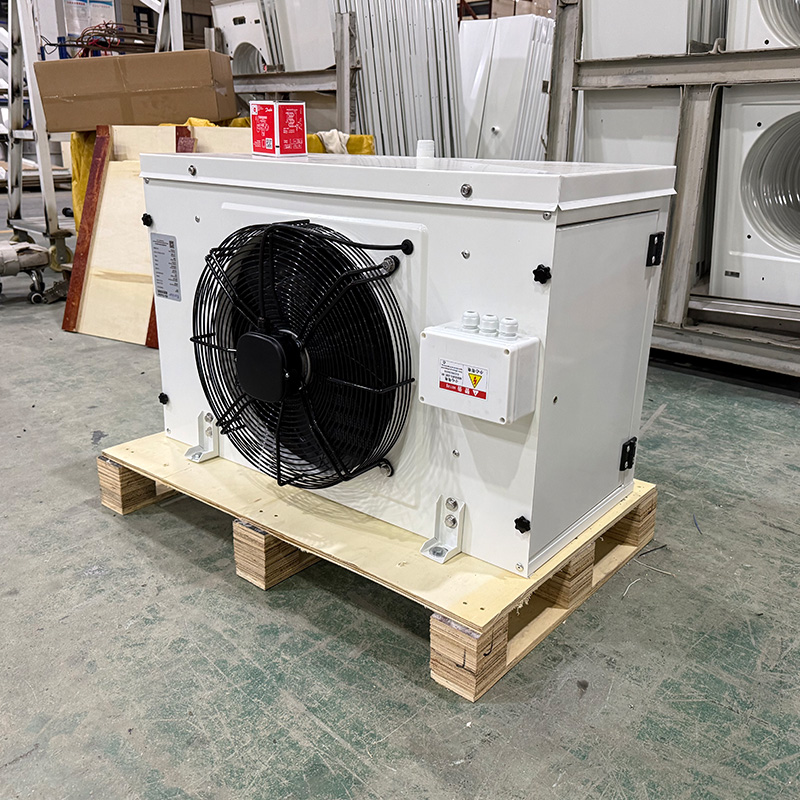
When evaluating suppliers for evaporator cold rooms, consider their manufacturing capabilities and experience. A supplier with over 20 years in the industry, like Shanghai EMTH, often possesses extensive knowledge of the market and can offer valuable insights into product selection and customization.
Examine the supplier's range of products and whether they can provide tailored solutions. Customization capabilities are essential, as they allow you to specify dimensions, materials, and additional features that meet your specific requirements. For example, they might offer advanced models like the Compressor For Refrigeration Tools And Equipment.
Another critical comparison factor is the supplier's quality assurance processes. Assess how they monitor and control the manufacturing process to ensure consistent product performance. Ask for details about their certifications, testing procedures, and any third-party validations they might have.
Pricing and lead time are also crucial factors. Suppliers may offer different pricing structures based on order quantity, so it’s beneficial to clarify minimum order quantities (MOQs) and potential discounts for bulk orders. Additionally, understanding their lead times can help you manage your inventory and supply chain more effectively.
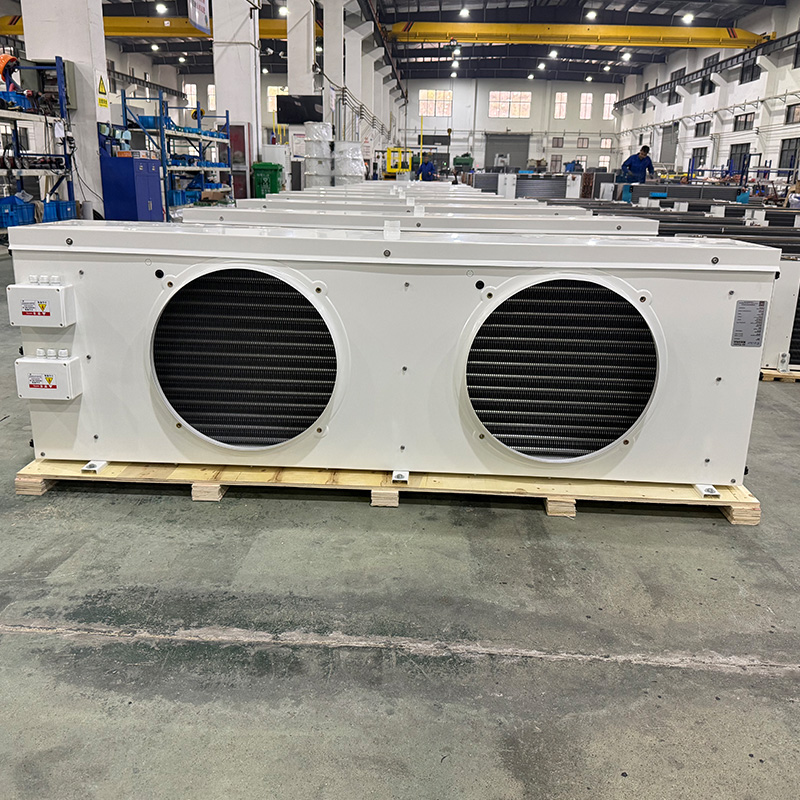
Finding trustworthy suppliers for evaporator cold rooms begins with thorough research. Start by exploring industry directories and trade associations relevant to refrigeration and cold storage. These platforms often feature verified manufacturers and suppliers.
Attending industry trade shows and exhibitions allows you to meet suppliers face-to-face, facilitating direct discussions about your needs and their capabilities. It also provides an opportunity to see their products in action and to gather insights from existing customers.
Online reviews and testimonials can also provide valuable information regarding the reliability and service quality of potential suppliers. Look for feedback regarding product performance, customer service, and post-sale support, as these factors can significantly affect your purchasing experience.
Once you have a shortlist of suppliers, consider requesting quotations. This process helps you compare not only pricing but also service terms, warranty offerings, and any additional support they provide.
A modern factory of over 40000 square meters is in place to satisfy the majority of Condensing units requirements.
More than 20 years of' experience and an experienced R&D EMTH team.
Special docking is offered to provide a full range of service. This includes the creation of Cuber ice machine, production installations, landing plans, and after-sales support.
EMTH has a long-standing track record of success in the industry with more than 3,000 satisfied customers.

Welcome to EMTH, a cold storage refrigeration equipment specialist in China! We offer innovative and effective cold storage solutions, including cold storage, evaporator, condensing unit and ice machine.
Room 304-305B, Building 5, BESHINE B.P, No. 559Zhuyuan Road, Minhang District 201112, Shanghai, China
Copyright © Shanghai EMTH Import & Export Co., Ltd. All Rights Reserved. - Privacy Policy
 EN
 AR
 BG
 HR
 CS
 DA
 NL
 FI
 FR
 DE
 EL
 IT
 JA
 KO
 NO
 PL
 PT
 RO
 RU
 ES
 TL
 IW
 ID
 LT
 SR
 VI
 HU
 TH
 MS
 AZ
 JW
 LO
 MN
 SO
 MY
 KK
 TG
 UZ
 GD
 XH